-
When This Checklist Applies
-
Step 1. Don’t Ask For “a Laser.” Name the Architecture.
-
Step 2. Measure the Beam With a Profiler. Don’t Just Read the Data Sheet.
-
Step 3. Answer “How Accurate Is CNC Turning?” per Feature, per Part.
-
Step 4. Organize Tools So a Wrong Tool Can’t Touch a Critical Part
-
Step 5. Cut One Test Coupon Before You Commit the Batch
-
Step 6. Require Actual Measurement Values, Not a “PASS” Stamp
-
Step 7. Turn Every Mistake Into a “Don’t Do This” Note
-
Additional Mistakes I Still Watch For
I manage process engineering for a shop that does laser micromachining, CNC turning, and light assembly. I’ve been handling custom fabrication orders for nine years, and I’ve personally made—and documented—11 significant mistakes, totaling roughly $22,000 in wasted budget. After the third rejected order in Q1 2024, I built the checklist below. As of January 2025, it has caught 47 potential errors before they became scrap.
When This Checklist Applies
Use this before any of these situations:
- Choosing a laser source for cutting, welding, marking, or micromachining.
- Accepting a beam-quality spec from a supplier instead of measuring it.
- Asking a job shop to hold tight tolerances on turned parts.
- Setting up a bench or cell where the wrong hand tool can ruin an expensive fixture.
It’s not a replacement for engineering judgment. It’s a way to slow down at the exact moment a mistake becomes expensive.
Step 1. Don’t Ask For “a Laser.” Name the Architecture.
Before we talk tolerances, there’s a language issue. If you write “coherent laser source” in an RFQ, every laser vendor will say yes—because every real laser is coherent by definition. That phrase tells a shop nothing about wavelength, pulse width, or power.
If you mean the OEM Coherent as a supplier, name the product family too. A Coherent Element laser—a Ti:sapphire-based ultrafast amplifier—is a completely different tool from a Coherent fiber laser built for marking plastic. I learned this in 2019 when I asked for a “precision laser” and got a nanosecond fiber laser for a micro-drilling job that needed femtosecond pulses. The heat damage was obvious on the first test coupon, but only after we paid for the wrong unit.
What to do:
- Write the material, thickness, feature size, and acceptable heat-affected zone.
- Specify wavelength and pulse width, not just brand.
- If you’re considering ultrafast processing, name the source architecture, e.g., a Ti:sapphire amplifier such as Coherent’s Element family.
Step 2. Measure the Beam With a Profiler. Don’t Just Read the Data Sheet.
Everything I’d read said an M² of 1.2 was fine for micromachining. For our first laser system it was not fine. The edges of a micro-channel looked wrong, but the power meter said we were getting full power. The issue was mode quality, not power.
We rented a Coherent Inc. laser beam profiler for two days. The setup took a few hours, and here’s what it showed: the real M² at focus was about 1.7, not the 1.2 on the data sheet. During those two days we also found the beam waist location was shifted by 4 mm from where the supplier said it should be. That explained why the process window was so tight.
If you don’t own a profiler, your checklist should include one of these:
- Rent one. Coherent Inc. laser beam profiler units are available through many industrial optics suppliers.
- Ask for the ISO 11146 measurement report from the laser vendor, including camera type, date, and calibration.
- Don’t run production until your own process tests match the beam data.
I only started believing beam-profile numbers after this mistake. Now it’s a gate, not an extra.
Step 3. Answer “How Accurate Is CNC Turning?” per Feature, per Part.
The question I get most is: how accurate is CNC turning? There’s no one number. Typical capability for standard CNC lathes on straightforward diameters is about ±0.005 in (0.13 mm). A good precision turning center can often hold ±0.001 in (0.025 mm) on qualified features. High-end Swiss-type or hard-turning setups may hold ±0.0002 in to ±0.0005 in (0.005 to 0.013 mm), but only in controlled conditions.
Those are real-world ranges, not promises. Accuracy depends on the feature, the material, the tooling, coolant temperature, and whether the part is rigid enough.
A drawing without geometric tolerances leaves all of that open. Many shops use general tolerances based on something like ISO 2768-m, and those general tolerances are much looser than people expect for a “precision” part. Put another way: if you don’t mark a feature as critical, don’t be surprised when it comes back at the general tolerance.
The machine can be accurate. The drawing is what tells it what to be.
What to include in every RFQ:
- A GD&T drawing or, at minimum, a list of critical diameters and true-position callouts.
- A note that the critical features must be measured and reported.
- The shop’s own QA procedure, including thermal compensation on long runs.
The $3,200 mistake I made was trusting that “CNC turning is accurate,” without saying which part feature mattered most. The vendor held the overall length to ±0.1 mm, but the press-fit diameter, the one that mattered, drifted. All 800 pieces were scrapped. That one cost us $2,100 in rework and a week of delay.
Step 4. Organize Tools So a Wrong Tool Can’t Touch a Critical Part
This sounds too basic for a laser/CNC checklist, but it isn’t. The most expensive error of 2022 in our shop wasn’t a beam profile or a CNC code problem. It was someone grabbing the wrong tool from a drawer full of sockets and torque adapters, then overtightening a fixture bolt on a $3,200 assembly.
We changed two things. First, the bench now has two pairs of VMC pliers: one for deburring and one for inserting snap rings. They’re marked with yellow heat-shrink and stored in one place on the wall grid; no one uses them for torque. Second, I modeled a tool-grid socket holder 3D print that separates metric and imperial sockets by size and drive. Each socket has its own hole. If one is missing, the empty hole tells us exactly where to look.
That whole project took an afternoon. It has saved far more than the $890 redo caused by the original drawer problem. Maybe you don’t think VMC pliers belong in a precision article. I’d argue the opposite: the wrong hand tool on a precision setup can do more damage than a slightly wrong spindle speed.
Step 5. Cut One Test Coupon Before You Commit the Batch
Laser parameters that work on last month’s material won’t always work on this month’s batch. Coatings, alloy variations, and surface finish can shift the process window.
Before a production run, we now cut or machine one coupon in the actual material and verify the critical feature. For a laser cut, that means checking taper, kerf width, and heat-affected zone under the microscope. For a turned part, it means measuring the critical diameter and surface finish at the same feed rate we intend to run.
It’s tempting to skip this step when the order is small. I’ve done it. That’s exactly when the material changes and the first real part ends up in the scrap bin.
Step 6. Require Actual Measurement Values, Not a “PASS” Stamp
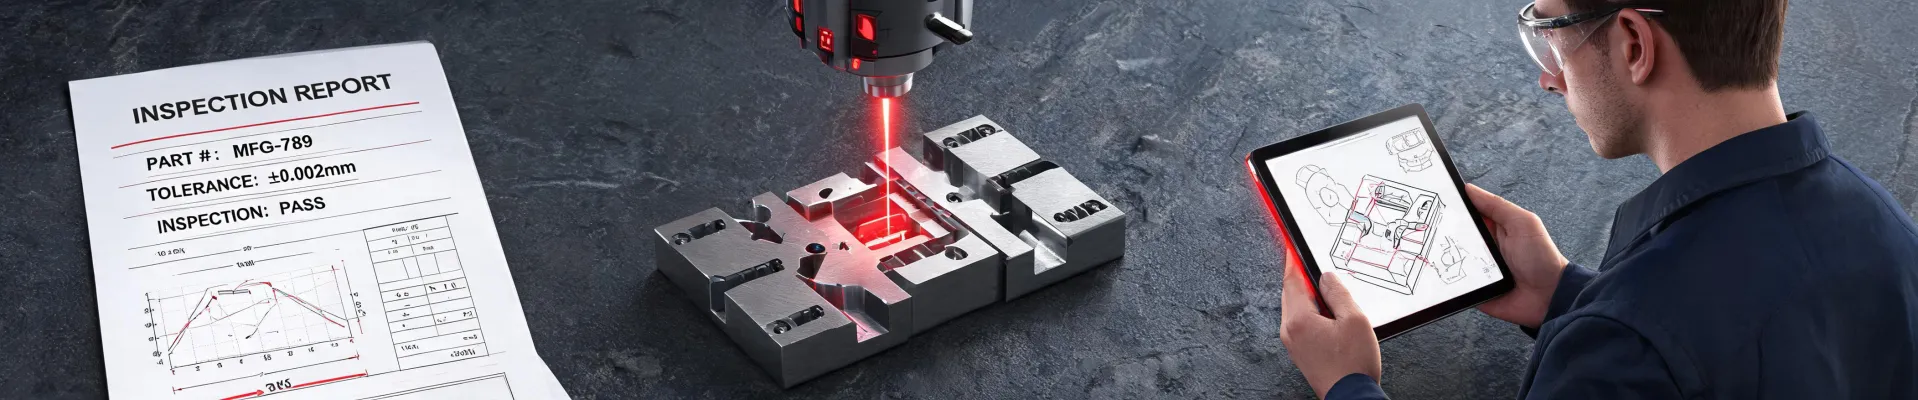
In Q1 2024, we received a laser-cut batch with a certificate that said “PASS.” Our customer measured a 12° taper where the drawing specified 5°. The certificate gave us false confidence—not because the supplier lied, but because someone in their QC workflow treated inspection as a checkbox instead of a measurement record.
Now every critical dimension requires an actual reported value:
- Beam diameter and M² where beam quality affects the process.
- Critical part diameters and true position for turned features.
- Taper or edge angle for laser-cut features.
If a supplier won’t provide measured values, I treat that as a risk signal. For 400-piece orders and up, we also ask for a copy of the CMM or micrometer report so we can archive it with the purchase order.
Step 7. Turn Every Mistake Into a “Don’t Do This” Note
The other six steps exist because of specific failures. The only way they stay effective is if every new error adds a line to the checklist. It sounds obvious, but most shops forget mistakes within two quarters. People leave, procedures fade, and the same expensive surprise comes back.
After an incident, we spend 20 minutes writing three things: what happened, what we assumed, and what check should have caught it. The checklist gets updated before the next order. If no one wants to own that task, the whole system decays.
Additional Mistakes I Still Watch For
Here’s what tends to go wrong even with a checklist:
- Assuming “laser marking” means the same thing as “laser engraving.” Depth requirements change the entire laser choice.
- Quoting a single CNC turning accuracy number without linking it to a feature size or material.
- Skipping beam profile checks on existing lasers after optics maintenance. Lenses get dirty, mirrors get bumped, and the beam changes even if the power setting doesn’t.
- 3D-printing holders and fixtures without considering their location. A PLA socket holder near a hot laser cell can sag over time.
- Using VMC pliers, or any pliers, as a substitute for a torque wrench.
Full disclosure: my experience is based on roughly 200 custom orders, mostly low-to-medium volume metal and glass work. If you’re doing high-volume aerospace parts or cutting thick steel plate, you’ll run into different failure modes. The discipline of slowing down before the purchase order is the part that transfers.
I’d rather spend ten minutes walking a customer through a laser spec than deal with mismatched expectations later. An informed customer asks better questions, and those questions always lead to faster decisions.