-
Step 1: Define the material as processed, not as named
-
Step 2: Separate laser type from laser power
-
Step 3: Put beam quality in the specification
-
Step 4: Validate on real production parts, not ideal coupons
-
Step 5: Audit the full process chain
-
Step 6: Write acceptance criteria before you run parts
-
The Checklist Has Limits
If you've been searching how thick can a laser welder weld, you probably noticed the answer changes depending on which page you land on. 3 mm. 10 mm. 30 mm. All of those numbers can be true, and none of them tell you whether a laser system belongs on your floor.
This checklist is for engineers, buyers, and shop managers evaluating an industrial laser for cutting, welding, or marking, especially when the parts are not clean flat sheet. It reduces the decision to six checks. In my experience, the last two checks are where most expensive surprises hide.
A quick note on perspective: I work in industrial laser quality at Coherent. I review system documentation and acceptance data before equipment ships, roughly 200 systems a year. In 2024, I rejected about 6 percent of first-pass acceptance packages because the written spec did not match measured beam behavior. So this comes from the side of the table that has to catch discrepancies before a customer does.
Step 1: Define the material as processed, not as named
Steel is not just steel. Annealed 304 stainless is a different thermal target than cold-rolled 304. A component made by metal injection molding behaves differently from machined bar stock with the same alloy name. The laser only sees the surface, but the surface remembers how the part was made.
If your parts are produced by amorphous metal injection molding, the cooling path is what creates the amorphous structure. That means downstream laser heating has a tighter thermal budget. A pulse sequence that forms a cosmetic mark on wrought metal can begin to change the structure in a bulk metallic glass. This is exactly the kind of detail that does not appear on a laser quote.
The same logic applies to tooling. A 20mm reamer bit that is solid carbide, carbide-tipped, or powdered HSS will respond differently to a marking laser. Coating type changes absorption first. If the reamer will be marked after grinding, confirm the coating and substrate before selecting pulse parameters.
Step 2: Separate laser type from laser power
The question how thick can a laser welder weld is usually treated as a watts question. In practice, it is a question about wavelength, pulse duration, beam quality, joint geometry, material state, shielding, and fixture stiffness.
Coherent makes CO2, fiber, and ultrafast lasers, so I am not forced to make one technology fit every problem. A Coherent fiber laser at the one-micron wavelength couples well into many metals. A CO2 laser is often a better fit for nonmetals that absorb the longer wavelength. Neither is universally superior.
When someone pushes for a number, I say this: a multi-kilowatt fiber laser can produce full-penetration welds in 10 to 12 mm steel in a single pass with proper joint preparation. Deeper sections can be welded with more power, multiple passes, or narrow-groove design. But that is a starting point, not a guarantee. The same laser can fail on 6 mm material if the edges are poor or the part moves during the weld.
Battery processing is where the type of laser matters even more than power. A Coherent femtosecond laser battery process uses pulses short enough to vaporize material before heat spreads into the surrounding foil. If the problem is heat-affected zone damage, increasing average power is the wrong answer. The answer is controlling the pulse duration.
Step 3: Put beam quality in the specification
Power is the easiest number to compare. Beam quality is the number that explains why one system produces a cleaner edge. Ask for the measured beam parameter product, not the best-case marketing value.
When I first started reviewing laser systems, I treated beam quality as a fixed characteristic. It is not fixed enough. It changes with power level, repetition rate, and the thermal state of the resonator.
One review stays with me. The application was a marking cell for cutting tools, and the target was a 20mm reamer bit. The spreadsheet said a 100 W fiber laser was adequate. The first samples looked good. My gut said we had not tested warm-up behavior, so I asked for a thirty-minute soak before the acceptance run.
The post-warm-up run showed a small beam drift. The part number was still readable, but the edge had a faint double trace that looked like a coating defect. We found it before shipment. The fix was not a different laser. It was a longer stabilization window and a beam monitoring check.
Step 4: Validate on real production parts, not ideal coupons
To be fair, coupon testing is faster and cheaper. It answers basic feasibility. It does not answer qualification questions.
A customer asked us to help with brackets made by amorphous metal injection molding. The failure mode was cracking near the hinge. The analysis pointed to a smaller, lower-cost laser because the material was only about 1.2 mm thick. My gut said to test the actual brackets, not the provided flat coupons.
The surprise was not heat input. The surface condition near the gate varied from shot to shot and changed the amount of laser energy absorbed. The coupon-based recommendation would have produced inconsistent welds. The final process added a surface-prep pass and a larger spot size to reduce sensitivity to oxide.
Step 5: Audit the full process chain
An industrial laser is one component in a process. The motion stage, clamping, assist gas, lens condition, cooling water, and exhaust all appear in the part quality.
- Measure assist gas pressure and flow at the nozzle, not at the regulator.
- Schedule optics inspection intervals. A compromised lens shifts the focus and can look like a beam quality defect.
- Check fixture rigidity under clamping load, especially for deep welds.
- Verify chiller temperature and flow before long production runs.
For thick-section welding, the limiting factor is often stability, not peak power. That is the real answer to how thick can a laser welder weld: it depends on how stable the full process is at a given thickness.
Step 6: Write acceptance criteria before you run parts
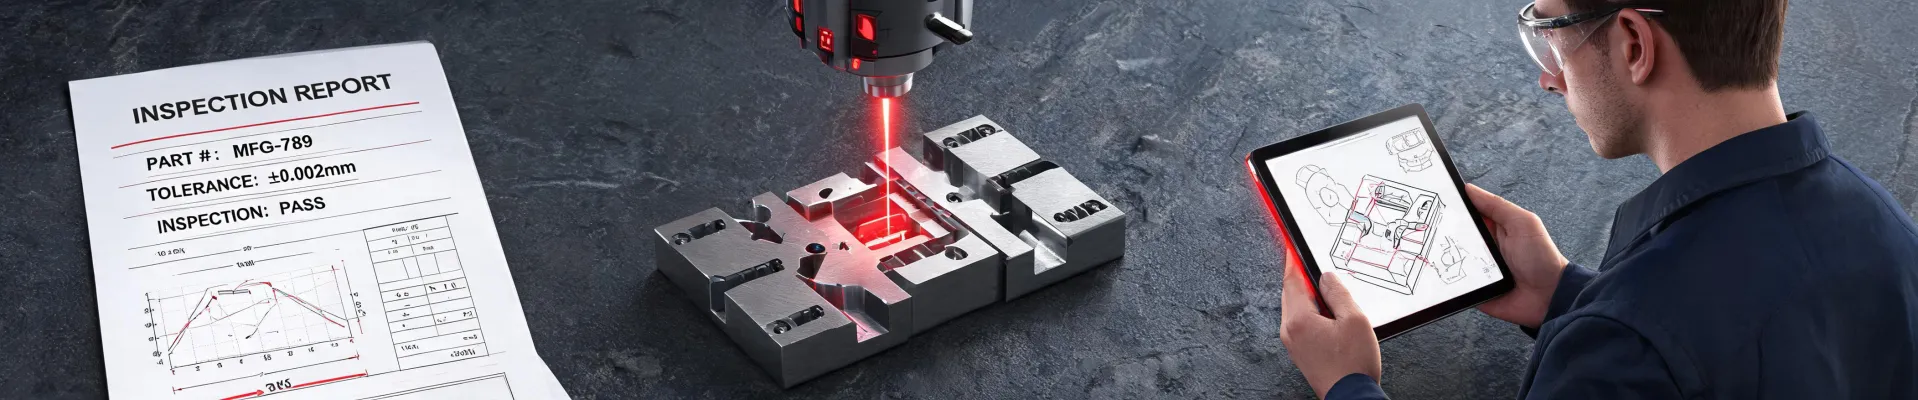
Before the first test, define what good looks like. Minimum penetration, maximum undercut, allowable heat-affected zone, mark contrast, burr height, edge condition on a 20mm reamer bit. If those numbers are not written down, visual acceptance will change as the schedule compresses.
One case where we got this wrong involved laser-marked tool blanks. The marking itself was clean, but the blanks were coated afterward, and the coating lifted along the edge of the mark. The burr was too fine to see on the bare substrate but enough to break the coating bond. The parts were reworked, and now first-article approval always includes the next operation.
In my opinion, this is the step people resist most because acceptance criteria expose unknowns. It is also the step that prevents the most expensive arguments.
The Checklist Has Limits
This evaluation method is not a reason to over-buy. If you weld mild steel occasionally and the weld is not structural, a fully integrated industrial system with femtosecond capability is overkill. The right laser is the one matched to your actual material, volume, tolerance, and process control.
If you process battery foil at high line speed, a Coherent femtosecond laser deserves serious evaluation, but only after you measure your heat-affected zone on the real stack. If your part comes from amorphous metal injection molding, verify the thermal sensitivity with your material supplier before you finalize the laser process.
OEMs like Trotec build systems around Coherent sources, and from my quality review seat that makes sense because the source behavior has to be repeatable across many installations. Even so, I do not promise maximum thickness or guaranteed cycle time before we run the customer's parts. The process validation is the only honest way to answer those questions.
This article is a starting point. If you remember one thing, remember that the laser alone is not the process. The material history, the beam path, the fixture, and the acceptance criteria all decide whether the weld or mark is acceptable.